Creator5
Creator5 Pro
Note
This document is relevant for Creator 5 and Creator 5 Pro
Important features
- The printer always works with 4 colors (T0, T1, T2, T3). All four slots are available in the selection menu.
- To turn on the camera, use
CAMERA_ON VIDEO=video67. - Klipper may crash. Solution:
Process Profile->Other->Output G-code->Exclude models— uncheck the checkbox. - Instead of the
CLOSE_DIALOGSmacro (slow closing), always useFAST_CLOSE_DIALOGS(fast closing). - The
NEW_SAVE_CONFIGmacro does not work. - No support for Klipper 13; contributions are welcome.
- On Creator 5 / Creator 5 Pro the Z-offset with the native screen and in screenless mode is the same — they are fully synchronized. If the native screen is disabled, you can change the Z-offset during printing via GuppyScreen, HelixScreen, Fluidd or Mainsail — it will be saved.
How to prepare a file in Orca
- Send files to print via Octo/Klipper.
- Orca Slicer Profiles
- It is strongly recommended to enable the preprocessor
COLOR
How to use the color and filament type selection menu
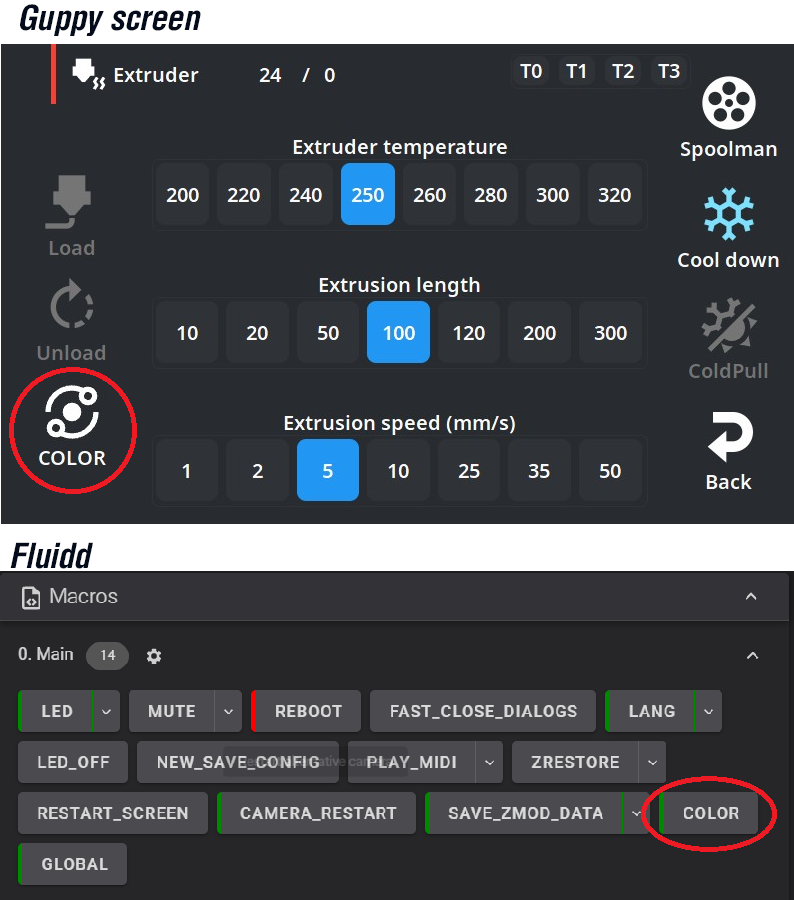
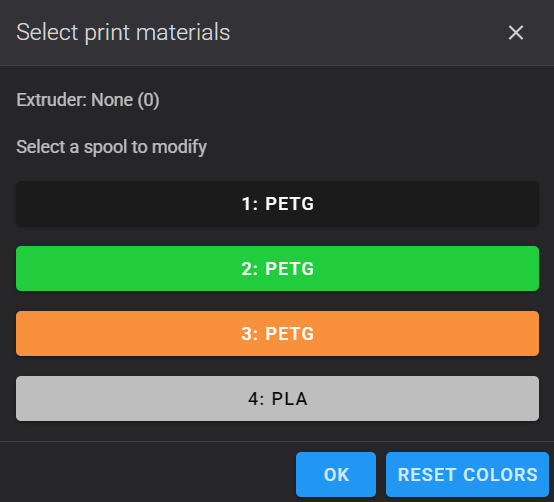
Select the spool you want to work with (for example, spool 2):
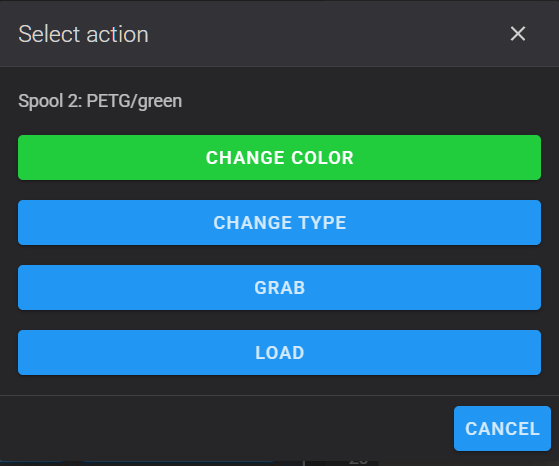
You can perform five actions:
- Change the spool color.
- Change the plastic type (PLA, PETG, ABS, ...).
- Pick up this extruder onto the carriage.
- Load new filament into the extruder.
- Remove this extruder from the carriage.
How to change color:
Click "Change color". Select a color from the list. This way the printer and the native screen will understand you best.
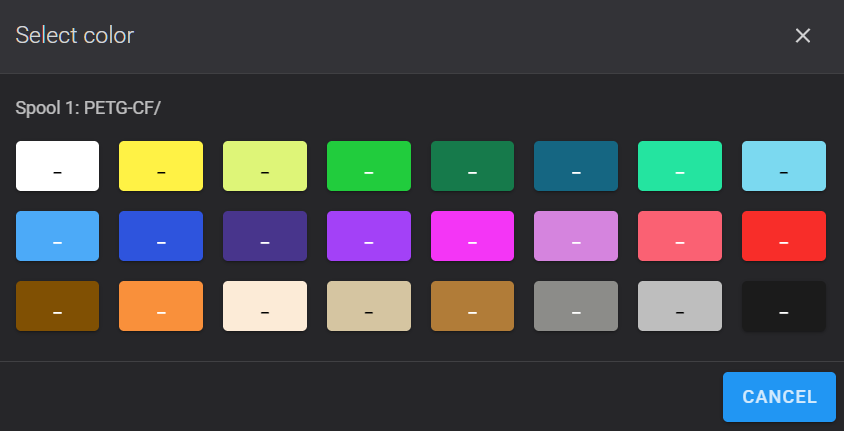
After selection you will return back, and the spool color in the list should change.
If the color did not change: close the window with the X and run the COLOR macro again. Sometimes the screen does not have time to refresh.
How to change type: Click "Change type". Select a type from the list. Types can be edited for screenless mode.
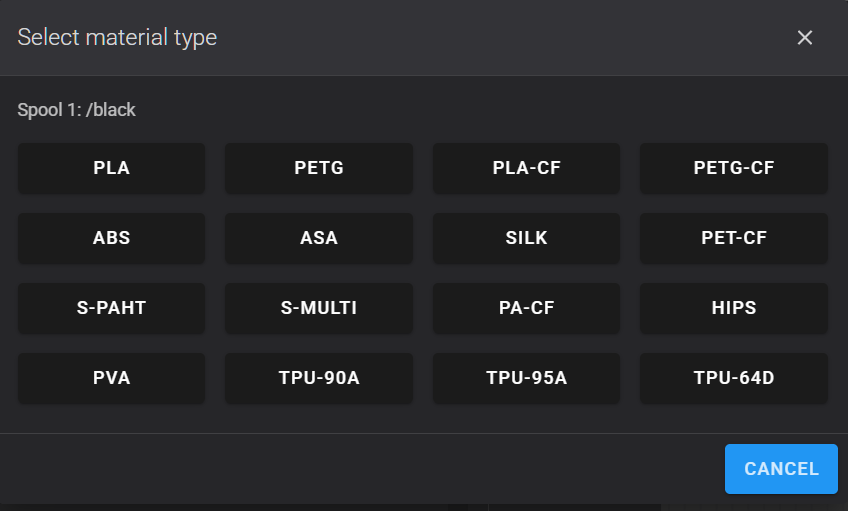
If the type did not change: close the window with the X and run the COLOR macro again. Sometimes the screen does not have time to refresh.
Tip: If several spools have the same color and type, the printer will automatically switch to the next spool when the first one runs out. This is called "endless spool mode".
PRINT
Print menu
This window opens automatically when you start printing, if the SAVE_ZMOD_DATA SILENT=0 parameter is set by default.
Alternative: with the ORCA_FF parameter, spools for colors are chosen right in OrcaSlicer or Flash Studio when sending a print.
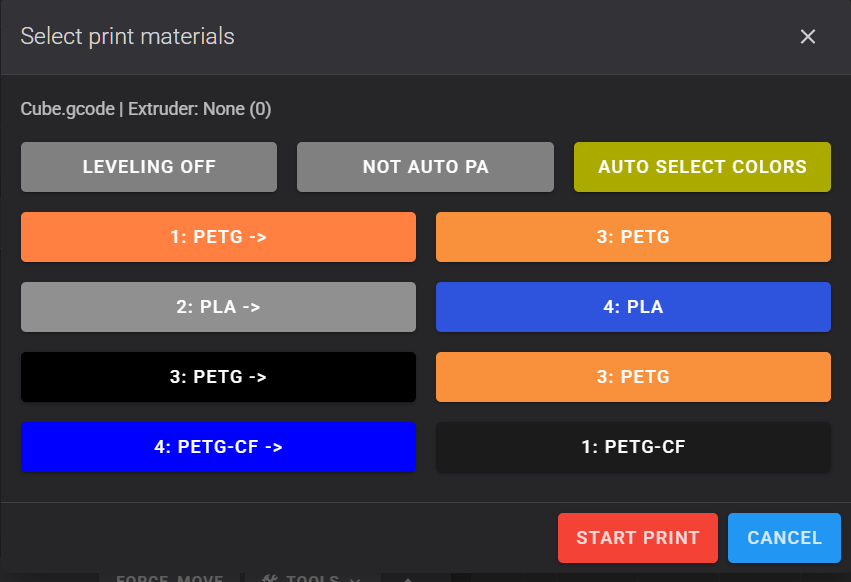
How to understand what is written here:
- In the left column are tool numbers and colors from the file passed from the slicer.
- In the right column are spool numbers and colors loaded/used on the printer.
Cube.gcode– this is the name of the file being printed.1: PETG ->– this is the first color from the file (orange PETG). It is printed with filament from spool 3 (orange PETG).2: PLA ->– this is the second color (gray PLA). It is printed with filament from spool 4 (blue PLA). Because there are no other PLA plastics in the printer.3: PETG ->– the third color (black PETG), printed from spool 3 (orange PETG). Because there are no other PETG plastics in the printer.4: PETG-CF ->– the fourth color (blue PETG-CF), printed from spool 1 (black PETG-CF). Because there are no other PETG-CF plastics in the printer.
If the image looks like this:
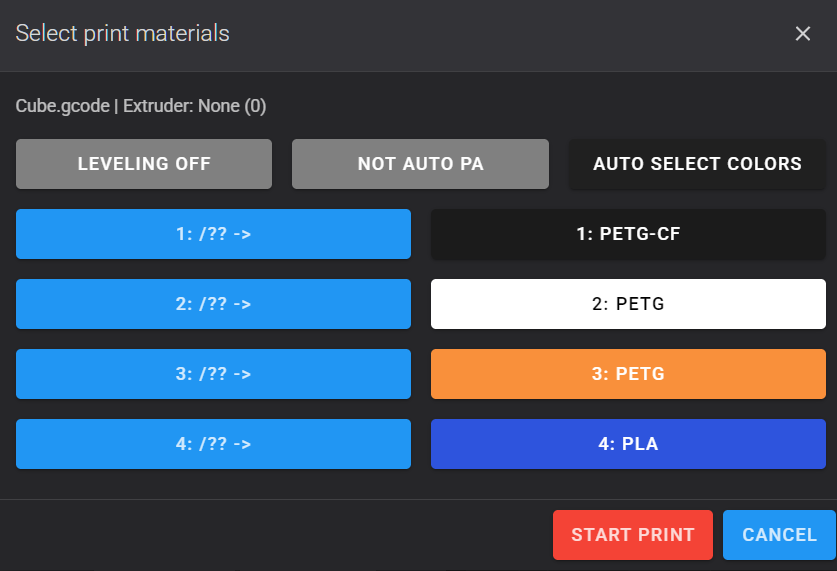
This means that you have disabled the auto color matching option and/or file scanning. You can click the AUTO_SELECT_COLORS button or enable it in global parameters:
SAVE_ZMOD_DATA SCAN_FILE_COLORS=1 AUTO_ASSIGN_COLORS=1
It is strongly recommended to enable the preprocessor
Bed mesh building and AUTO PA
There are two important buttons in the print menu:
Leveling (Bed mesh):
Probe bed mesh— before printing, automatic bed mesh building will be performed.Do not probe bed mesh— the previously saved mesh will be used.
Auto PA (Automatic Pressure Advance selection):
- If the
Auto PAbutton is active (green), then before printing the printer will automatically select the optimal Pressure Advance value for each used extruder. - The process takes several minutes, but significantly improves the quality of corners and thin elements.
- If
Auto PAis off, the PA values from the slicer will be used.
Note
By default the calibration runs from 0.010 to 0.040 in 0.005 steps, in 3 passes. For viscous plastics such as PETG the range can be widened in mod_data/user.cfg, for example:
[zmod_color]
pa_min: 0.010
pa_max: 0.080
pa_count: 3
pa_min— lower bound, at least 0.01 (default 0.010)pa_max— upper bound, from 0.02 to 0.100 and not less thanpa_min(default 0.040)pa_count— number of passes, from 1 to 10 (default 3)
The step is fixed: 0.005. The wider the range and the more passes, the longer the calibration.
Purging all extruders without Auto PA. By default only the first extruder is purged at print start. To purge all used extruders, enable the global parameter PURGE_ALL_EXTRUDERS: SAVE_ZMOD_DATA PURGE_ALL_EXTRUDERS=1
Fine tuning
Does not work with the factory screen view, so you first need to turn off the native printer screen using the DISPLAY_OFF macro.
How to find these settings:
- Click the "Configuration" tab.
- Find and open the
mod_datafolder. - In this folder, find and open the
filament.jsonfile.
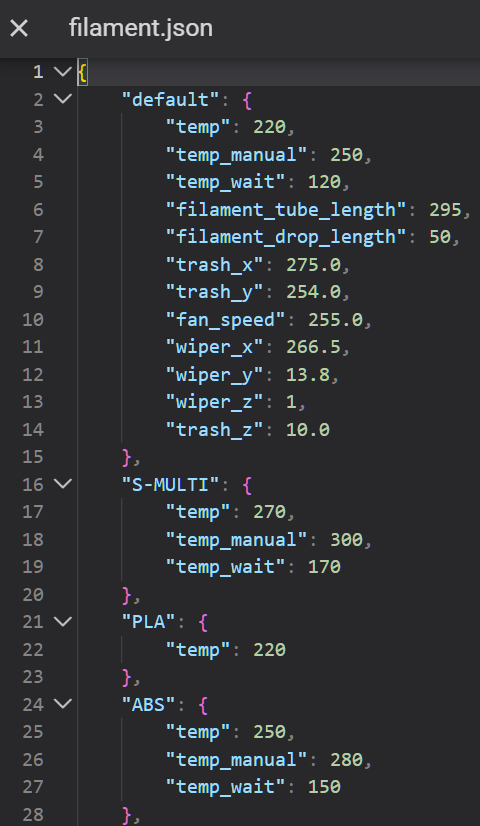
In this file, for each plastic type (PLA, ABS, PETG, etc.) there is a list of numbers. Here is what they mean:
| Parameter | Default | Description |
|---|---|---|
temp |
220 | Temperature to which the nozzle is heated to change filament. The value depends on the material type |
temp_manual |
250 | Purge temperature in manual mode (when loading through the menu). |
temp_wait |
120 | Idle temperature — the nozzle cools down to it after purging. |
filament_drop_length |
50 | Drop length. How many millimeters of plastic the printer will extrude into the trash bin before printing; 0 disables moving to the trash bin. |
filament_full_length |
600 | Tube length. How many millimeters of plastic the printer will extrude after the filament runout sensor triggers |
filament_tube_length |
295 | Filament loading length when inserting a new spool. |
Default temperatures for different materials:
| Material | temp |
temp_manual |
temp_wait |
|---|---|---|---|
| PLA | 220 | 250 | 120 |
| PETG | 240 | 270 | 140 |
| PLA-CF | 220 | 250 | 120 |
| PETG-CF | 240 | 270 | 140 |
| ABS | 250 | 280 | 150 |
| ASA | 250 | 280 | 150 |
| SILK | 220 | 250 | 120 |
| PET-CF | 270 | 300 | 170 |
| S-PAHT | 280 | 310 | 180 |
| S-MULTI | 270 | 300 | 170 |
| PA-CF | 270 | 300 | 170 |
| HIPS | 250 | 280 | 150 |
| PVA | 220 | 250 | 120 |
| TPU-90A | 220 | 250 | 120 |
| TPU-95A | 220 | 250 | 120 |
| TPU-64D | 220 | 250 | 120 |
Advanced parameters
| Parameter | Default | Description |
|---|---|---|
trash_x |
275.0 | X coordinate of the trash bin. |
trash_y |
254.0 | Y coordinate of the trash bin. |
trash_z |
10.0 | Z coordinate of the trash bin. |
wiper_x |
266.50 | X coordinate of the nozzle cleaning place (rubber). |
wiper_y |
13.80 | Y coordinate of the nozzle cleaning place. |
wiper_z |
1.0 | Z coordinate of the nozzle cleaning place. |
fan_speed |
255.0 | Fan speed (from 0 to 255) when cooling the nozzle after purging. |
Warning! Changing parameters in the advanced section may lead to incorrect printer operation, filament jams or breakdowns. Change them only if you fully understand what each parameter is responsible for and what the consequences may be.
Global parameters
To prevent the color selection window from showing at the start of printing, use the global parameter
SILENT:
- 0 — show the window (default)
- 1 — do not show the window, use previously set colors
- 2 — do not show the window; if auto-matching fails, show the selection menu
SAVE_ZMOD_DATA SILENT=1
To enable scanning of gcode files for information about tools, colors and materials, use the parameter SCAN_FILE_COLORS.
SAVE_ZMOD_DATA SCAN_FILE_COLORS=1
0 — disable the parameter
- 1 — full scan of the Gcode file
- 2 — check only the data prepared by the slicer script, without scanning the entire file
!If file scanning is disabled, the printer does not know how many extruders are used, so Auto PA will be run for all spools
Note
For 3MF files, auto-matching and scanning are enabled automatically
To enable automatic color matching from the gcode file with physical spools, use the parameter AUTO_ASSIGN_COLORS. For this function to work, file scanning must be enabled.
SAVE_ZMOD_DATA AUTO_ASSIGN_COLORS=30
1 — printing continues even if auto color assignment failed
- 2 — At least one material does not match (for example, gcode says ABS, but you only have PLA loaded)
- 4 — At least one color does not match at all (usually because file scanning is disabled)
- 8 — At least one color matches poorly
- 16 — The same physical spool was assigned to more than one tool index in the file
For example, using the value 30 will abort printing in silent mode if any problems with automatic assignment occur, and AUTO_ASSIGN_COLORS=6 (2+4) will abort printing if at least one material does not match + at least one color does not match at all.
Note
For 3MF files, auto-matching and scanning are enabled automatically
To automatically turn off heating of unused extruders during multi-color printing, use the parameter unused_extruders_off_time. It sets the timeout (in minutes) after which an idle tool will be turned off to avoid filament degradation and idle operation.
SAVE_ZMOD_DATA unused_extruders_off_time=5
Details: UNUSED_EXTRUDERS_OFF_TIME.
You can set the following values (in minutes):
* 0 — function disabled (extruders do not turn off during idle)
* 5, 10, 20, 40, 60 — time after which the unused extruder will be turned off
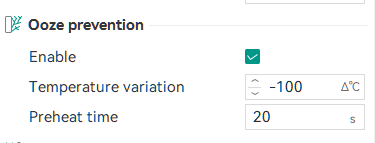
Important: For this option to work correctly, Ooze prevention must be enabled in the slicer (Print settings > Multimaterial > Ooze prevention). Without it, the printer cannot correctly handle the temperature modes of idle hotends during filament change.
Shapers from Klipper 13 are enabled by the parameter:
KLIPPER_C5:
0— do not use (default).1— use shapers from Klipper 13.
SAVE_ZMOD_DATA KLIPPER_C5=1
Change the number of attempts to pick up or put back the tool
In the Fluidd web interface, open mod_data/user.cfg via "Configuration" in the left column and add the lines:
[zmod_color]
retry: 3
Default is 5. [Sections] and macros in this file are not changed by firmware updates.
Filament sync with OrcaSlicer
Does not work with the factory screen view, so you first need to turn off the native printer screen using the DISPLAY_OFF macro.
The orca_lanes parameter publishes the extruder slots to the Moonraker database. OrcaSlicer reads filament color and type from there for the "Sync filament" button when the printer is added via Octo/Klipper (agent Moonraker) or via the FlashForge type.
True- publish slots (default)False- do not publish
If colors are managed by HelixScreen (helix = 1), publishing is skipped regardless of orca_lanes, so its data is not overwritten.
To disable, add to mod_data/user.cfg:
[zmod_color]
orca_lanes: False
Details
Slots are written to the lane_data namespace in the same format as AFC and Happy Hare: slot 1 → lane0, …, slot 4 → lane3, for example "lane0": {"lane": "0", "material": "PETG", "color": "#161616", "name": "PETG"}. All slots are published when Klipper starts, then only the changed slot on every color or type change. A slot with type ? is removed, filament presence from sensors is not taken into account. The color matched to the printer palette is sent.
AFC panel
The IFS slots (AD5X) and toolheads (Creator 5 Pro) are shown in Fluidd and Mainsail as a standard AFC panel. Works both with and without the native screen.
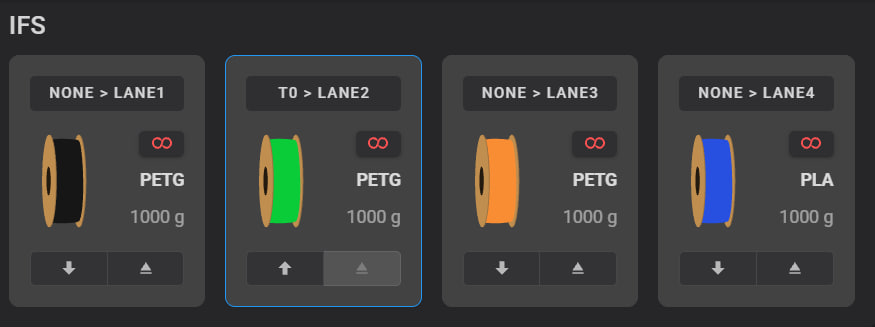
Enabling
SAVE_ZMOD_DATA AFC=1, then restart Klipper. To disable: SAVE_ZMOD_DATA AFC=0.
Features
- Color, type and filament presence in each slot.
- Change color and type, load and unload right from the panel.
- Lane selection window before printing in Fluidd (1.37.3+) and Mainsail: the mapping of file tools to slots is sent together with the print command, and the color selection window does not appear after it. The map is kept between prints and can be changed during a print as well.
- The AFC window has "Bed mesh" and "Auto PA" (Creator 5 Pro only) toggles. They change the global settings immediately, before you press "Print".
- Printing via the FlashForge protocol (OrcaSlicer, Flash Studio) uses the mapping from the slicer and starts right away, with the usual preparation (KAMP, MD5 check).
- Printing without a mapping (OrcaSlicer via Moonraker, GuppyScreen, KlipperScreen, macros) shows the color selection window or runs automatic matching, depending on the settings, just as without AFC.
- The infinite spool button reports that the replacement is picked by filament type and color.
zmod_afclite plugin
The zmod_afclite plugin has been removed and replaced by built-in AFC support. On update:
- if the plugin was enabled, it is disabled and AFC is enabled automatically;
- the plugin is removed from the Moonraker configs and its directory is deleted.
Acknowledgements
Thanks to DIEHARDave for the zmod_afclite plugin, which showed the way and the solution.
Add your own filament types
For these settings to work, you need to turn off the native printer screen using the DISPLAY_OFF macro.
To add a new filament type, add to mod_data/user.cfg:
[zmod_color]
filament_NEWTYPE: 300
Where NEWTYPE is replaced with the desired filament type (for example HIPS), and the number is the extruder temperature for loading, unloading and purging this filament. Based on this value, temp_manual (+30) and temp_wait (−100) will be automatically calculated.
To hide a filament type, add to mod_data/user.cfg:
[zmod_color]
hide_filament_types: XXX,YYY,ZZZ
Where XXX, YYY, ZZZ are replaced with the desired filament types (for example PLA-CF,PETG-CF,SILK). This can be used to hide default types or types you added manually. The filament type is not disabled, only hidden in the type selection menu.
Add your own colors
For these settings to work, you need to turn off the native printer screen using the DISPLAY_OFF macro.
To add or rename a color, open mod_data/color/en.json (use your language instead of en) and add a new color or rename an existing one.
For the color name to be displayed, the color name must start with an underscore _.
Example:
{
   "ffffff": "white",
   "fffff1": "_transparent",
   "fef043": "bright yellow",
   "dcf478": "light green",
   "0acc38": "green",
   "067749": "dark green",
   "0c6283": "blue-green",
   "0de2a0": "turquoise",
   "75d9f3": "light blue",
   "45a8f9": "blue",
   "2750e0": "dark blue",
   "46328e": "purple",
   "a03cf7": "bright purple",
   "f330f9": "magenta",
   "d4b0dc": "lilac",
   "f95d73": "pink",
   "f72224": "red",
   "7c4b00": "brown",
   "f98d33": "orange",
   "fdebd5": "beige",
   "d3c4a3": "light brown",
   "af7836": "terracotta",
   "898989": "gray",
   "bcbcbc": "light gray",
   "161616": "black"
}
The label _transparent will be displayed on the buttons.
Extruder calibration
Works only without the native screen (
display_offmode).
Extruder calibration allows the printer to know the exact position of each of the four nozzles relative to each other. This is necessary for high-quality multi-color printing.
When to calibrate: - After replacing or repairing an extruder. - If you notice that colors do not align on the model (offset in X, Y or Z).
How to run:
- Remove the build plate from the bed!
- Run the
CALIBRATE_EXTRUDERSmacro from the menu or enter in the console:CALIBRATE_EXTRUDERS - A confirmation window will appear. Click
OK.
What will happen:
- The printer will perform homing (G28).
- Heat the bed to 65°C.
- Take each of the 4 extruders (T0–T3) in turn.
- For each extruder: heat the nozzle, perform a purge, clean against the rubber, then use sensors to determine the exact X, Y and Z coordinates.
- The results are automatically written to
rw/extruder.json. - At the end, the printer will output the found offsets for each extruder to the console.
Additional parameters (for advanced):
| Parameter | Default | Description |
|---|---|---|
BED_TEMP |
65.0 | Bed temperature during calibration |
SEARCH |
14.0 | Sensor search radius (mm) |
HOVER |
0.6 | Hover height above the point |
SAFE_Z |
10.0 | Safe Z height |
Example with parameters:
CALIBRATE_EXTRUDERS BED_TEMP=70 SEARCH=12
Warning! Do not interrupt calibration. The process takes several minutes.
VFA calibration
Works only without the native screen (
display_offmode).
VFA (Vertical Fine Artifacts) calibration allows reducing vertical artifacts on the print surface caused by stepper motor resonances.
How to run:
Enter in the console:
CALIBRATE_VFA T=0
Where T=0 is the extruder number (0–3) that will be used during calibration.
What will happen:
- The printer will take the specified extruder.
- Reset all G-code offsets.
- Move the head to the bed center (X130 Y130).
- Run automatic resonance calibration (
STEPPER_RESONANCE_FACTORY_CALIBRATE). - Return the extruder to its place.
- Save the configuration (
SAVE_CONFIG).
Tip: It is recommended to perform VFA calibration when visible vertical stripes appear on the print surface.
T_INFO macro
The T_INFO macro shows the current state of all extruders and printer sensors.
How to run:
T_INFO
What will be output to the console:
// T0: home
// T1: HEAD
// T2: home
// T3: home
// Door: Close
// Top: Close
// Offset: X=0.000 Y=0.000 Z=0.061 (0.000)
How to read:
home— the extruder is in its place (in the parking pocket).HEAD— the extruder is installed on the print head.?— undefined state (sensors did not trigger).ERROR (both)— error: the extruder is both home and on the head (sensor desync).Door— front door state (Close/Open).Top— top cover state (Close/Open).Offset— current G-code offsets along the X, Y, Z axes.
Ventilation modes
Creator 5 Pro is equipped with a chamber ventilation system with several fans. Proper ventilation control is critically important for the print quality of different materials.
External intake (PLA, TPU):
The AIR_CIRCULATION_EXTERNAL macro turns on chamber exhaust and fresh air supply. It is needed for PLA and TPU so the plastic cools quickly and does not soften from chamber heat.
AIR_CIRCULATION_EXTERNAL
chamber_fan (exhaust) | 0.5 |
| chamber_cool_fan (cooling) | 0.7 |
| chamber_heat_fan (heating) | 0.0 |
| chamber_loop_fan (circulation) | 0.0 |
Internal circulation (ABS, ASA):
The AIR_CIRCULATION_INTERNAL macro turns on internal circulation and chamber heating. It is needed for ABS and ASA to avoid delamination and warping from temperature changes.
AIR_CIRCULATION_INTERNAL
chamber_fan (exhaust) | 0.0 |
| chamber_cool_fan (cooling) | 0.0 |
| chamber_heat_fan (heating) | 0.9 |
| chamber_loop_fan (circulation) | 0.3 |
Stopping ventilation:
The AIR_CIRCULATION_STOP macro completely turns off all chamber fans.
AIR_CIRCULATION_STOP
Where to add ventilation macros
Recommendation: It is best to add ventilation macro calls to the filament code in the slicer. This will ensure automatic mode switching when the material changes.
In OrcaSlicer:
- Open filament settings.
- Go to the "Filament Settings" tab.
- In the Filament start G-code field, add the needed macro:
- For PLA:
AIR_CIRCULATION_EXTERNAL- For ABS:AIR_CIRCULATION_INTERNAL- For TPU:AIR_CIRCULATION_EXTERNAL
Example for PLA:
; Filament start gcode
AIR_CIRCULATION_EXTERNAL
Example for ABS:
; Filament start gcode
AIR_CIRCULATION_INTERNAL
Thus, during multi-color printing with different materials, ventilation will automatically switch to the required mode for each extruder.
Print acceleration
To disable the firmware slowdowns on short perimeters, open the Fluidd web interface -> left column -> Configuration tab -> mod_data/user.cfg and add three lines:
[printer]
short_move_limit: False
short_extrude_move_limit: False
Starting with factory firmware 1.9.9, this setting significantly speeds up printing, but can cause printer crashes when printing with fuzzy skin.
Disabling fast head return and preheating
Add to mod_data/user.cfg:
[virtual_sdcard]
enable_speed_return: False
enable_preheat: False
- enable_speed_return:
enable_speed_return: False— the head returns to the model from the hotend pickup area at the speed and along the trajectory set in the slicer.enable_speed_return: True— the head returns to the model from the hotend pickup area at 600 mm/s along a trajectory chosen by the printer firmware (collisions with the edges of the prime tower are possible).
- enable_preheat:
enable_preheat: False— disables predictive background scanning of the G-code file during printing, unloading the CPU and disk. Predictive heating is calculated more accurately on the OrcaSlicer side.enable_preheat: True— uses predictive background scanning of the G-code file to preheat the next nozzle. Speeds up heating when more than two nozzles are used within a short time, since the printer cannot heat more than two nozzles simultaneously.
Disabling the open door notification
To remove notifications about an open cover or door in screenless mode:
Add to mod_data/user.cfg:
[gcode_button topDoor]
press_gcode:
release_gcode:

[gcode_button frontDoor]
press_gcode:
release_gcode:
Disabling the color selection window when inserting filament
To stop the color and type selection window from appearing when filament is inserted in screenless mode:
Add to mod_data/user.cfg:
[gcode_macro _SENSOR_INSERT_HANDLER]
gcode: